 S M OpticalsSpectacle Frame Manufacturer · India
Sales Desk+91-8047836571
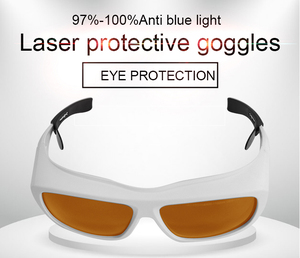
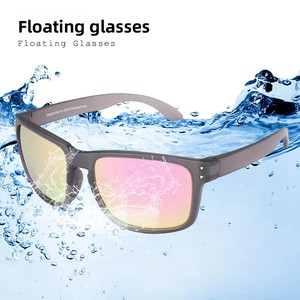
S M OpticalsSpectacle Frame Manufacturer · India Explore our verified manufacturing inventory covering specialized protective eyewear, floating maritime frames, ultra-resilient youth opticals, and statement oversized geometries.
Scaling up lens diameters without introducing optical aberration or center-of-gravity imbalance requires specialized cantilever geometry, tailored pantoscopic tilt, and next-generation polymer substrates.
Oversized frames naturally exaggerate peripheral vertex distance. In our China-based manufacturing hubs, our tooling masters calibrate the pantoscopic angle between 7° and 9°, neutralizing visual distortion on freeform prescription lenses while preserving a bold aesthetic silhouette.
Large-format acetate designs often induce bridge slippage. By precision-milling variable rim thickness—slimming from 6.0mm top rims to 3.2mm lower rims—we shift the frame center-of-gravity backward toward the auricular temporals, maximizing long-duration wearing comfort.
To eliminate temple deformation on wide frame profiles, we integrate custom-milled stainless steel and nickel-silver core-wires. Each wire is etched with micro-grooving to bond permanently with high-density cellulose acetate during thermal lamination, ensuring lifetime frame retention.
Choosing the right substrate determines yield rate, finishing luster, hinge stability, and end-consumer satisfaction across varied global climatic zones.
| Material Classification | Specific Gravity | Tensile Strength (MPa) | Thermal Stability | Optimal Global Application |
|---|---|---|---|---|
| High-Density Cellulose Acetate | 1.28 – 1.32 g/cm³ | 85 – 105 MPa | Glass transition at 115°C | Luxury fashion oversized spectacles, rich tortoise layers, deep bevel hand-polished frames. |
| Swiss EMS Grilamid TR90 | 1.02 g/cm³ | 60 – 75 MPa | Stable up to 135°C | Ultra-lightweight large frames, sports lifestyle, unbreakable pediatric and teen opticals. |
| TPX (Polymethylpentene) | 0.83 g/cm³ | 25 – 35 MPa | Melting point 235°C | True-buoyancy floating water sports frames, marine-grade polarized sunglasses. |
| Optical-Grade Monel / Stainless Steel | 8.80 / 7.90 g/cm³ | 450 – 700 MPa | High resistance > 350°C | Thin-wire retro oversized pilots, combination frames with nylon supra cord mounts. |
Forward-looking intelligence for chain store buyers, private label brands, and multinational optical distributors.
International retail chains are mandating non-phthalate plasticizers and bio-based carbon contents exceeding 68% (derived from cotton linters and wood pulp), driving green procurement protocols in international optical supply.
The oversized frame footprint offers the ideal volumetric cavity to embed bone-conduction transducers, micro-directional microphones, and extended battery modules without disrupting exterior aesthetics.
With advanced 5-axis CNC router lines, upfront prototyping lead-times have compressed from 45 days down to 7 days, allowing private labels to launch seasonal micro-batches with minimal inventory overhead.
Comprehensive compliance covering ISO 12870, EU 2017/745 (MDR Class I for corrective frames), ANSI Z80.5, and FDA registration has become an indispensable baseline for cross-border optical entry.
Rooted in complete industrial chain integration—from raw material tumbling, tool-and-die fabrication, high-precision automated milling, to 72-hour robotic drum polishing—we engineer reliable optical excellence. We remove trading friction, offering direct-from-facility accountability with verifiable traceability.
Contact UsClear answers to technical specifications, minimum order constraints, mold tooling fees, and global export compliance.
For customized acetate frames requiring custom-extruded sheet patterns, our baseline MOQ is typically 300 to 500 pieces per colorway. For injection-molded TR90 or PC models, standard MOQ is 1,200 pieces per mold, with flexibility across 3 to 4 customized color coatings.
Oversized frames have greater surface area and leverage stress. We apply internal stress-relieving annealing cycles to acetate blanks prior to milling. Furthermore, export packaging utilizes custom form-fitting EPS trays preventing lateral torsional stress during ocean and air transit.
Yes. Our ophthalmic frames intended for prescription corrective lenses comply with EU Regulation 2017/745 (Class I Medical Devices). We issue complete Technical Documentation files, Declarations of Conformity, and ISO 12870 test reports covering nickel release, biocompatibility, and flammability.
High-fidelity SLA/CNC rapid prototypes take 7 to 10 working days. Steel injection mold fabrication spans 30 to 35 days. Upon sample approval, mass production typically completes in 45 to 60 days depending on the complexity of hand-polishing and multi-barrel hinge assembly.
Partner with an established Chinese manufacturing leader. Connect directly with our optical engineering team to request factory pricing, material swatches, and mold evaluation.
Contact Us