 S M OpticalsSpectacle Frame Manufacturer · India
Sales Desk+91-8047836571
S M OpticalsSpectacle Frame Manufacturer · India From architectural luxury displays to heavy-duty industrial chassis mounting systems, explore our factory-direct stainless steel fabrication assemblies manufactured to rigorous European technical tolerances.
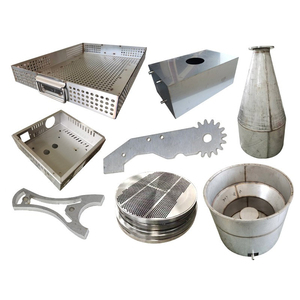
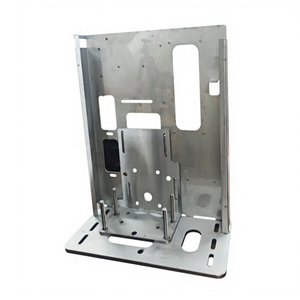
In international engineering and precision architectural hardware procurement, acquiring stainless steel frames transcends basic aesthetic preferences. Compliance with the European Union Construction Products Regulation (CPR No 305/2011) and EN 1090-2 (Execution of steel structures and aluminum structures) demands uncompromising metallurgical consistency, documented traceability, and validated weld integrity. As a leading manufacturer and exporter, our CE-marked stainless steel framing systems undergo strict Factory Production Control (FPC) procedures, verifying mechanical ductility, impact toughness at cryogenic and elevated temperatures, and microscopic grain boundary stability against intergranular corrosion.
Our manufacturing infrastructure utilizes prime-grade austenitic stainless steel (primarily AISI 304, 304L, 316, and 316L according to ASTM A240 / EN 10088-2) as well as cost-effective ferritic (AISI 430) and high-yield duplex alloys (2205 / EN 1.4462). Each alloy undergoes chemical spectrum verification before entering the CNC laser cutting and robotic forming line. Unlike commercial generic fabricators who risk carbon cross-contamination, our workshop maintains strict segregation of stainless and carbon processing zones to eliminate galvanic cell ignition and surface oxidation pits.
Procurement engineers must balance corrosion performance, yield strength, formability, and total cost of ownership. The comparative engineering matrix below outlines our standard alloy specifications deployed across commercial architectural framing, medical-grade cleanroom framing, and industrial machine chassis fabrication:
| Stainless Steel Grade | EN / DIN Equivalent | Yield Strength (Rp0.2, MPa) | Tensile Strength (Rm, MPa) | Pitting Resistance (PREN) | Primary Application Profile | Compliance Status |
|---|---|---|---|---|---|---|
| AISI 304 (V2A) | 1.4301 / X5CrNi18-10 | ≥ 230 | 540 – 750 | 18.0 – 20.0 | Indoor architectural frames, retail displays, decorative casing | CE / RoHS / REACH |
| AISI 304L (Low Carbon) | 1.4307 / X2CrNi18-9 | ≥ 220 | 520 – 700 | 18.0 – 20.0 | Heavy welded structural frames, deep drawing, chassis casing | CE / EN 1090-2 |
| AISI 316L (Marine Grade) | 1.4404 / X2CrNiMo17-12-2 | ≥ 240 | 530 – 680 | 23.1 – 26.5 | Coastal facades, marine equipment frames, chemical washdown skids | CE / DNV Certified |
| Duplex 2205 | 1.4462 / X2CrNiMoN22-5-3 | ≥ 450 | 680 – 880 | 32.0 – 36.0 | Heavy dynamic load supports, offshore frames, structural columns | CE / ISO 15156 |
| AISI 201 (Economy Series) | 1.4372 / X12CrMnNiN17-7-5 | ≥ 310 | ≥ 650 | 14.0 – 16.0 | Internal consumer goods, lightweight art frames, dry interior decor | Factory Verified |
Our production facilities combine advanced European-calibrated CNC machinery with certified welding and polishing protocols. As a specialized manufacturer operating directly under international export audits, our facility enforces end-to-end quality assurance across every phase of frame fabrication:
Equipped with 15kW ultra-high-speed fiber laser cutters utilizing nitrogen assist gas. We achieve 100% oxide-free, burr-free cuts on sheets and tubes up to 25mm thickness, eliminating the need for costly secondary de-burring.
Multi-axis dynamic crowning press brakes ensure precise angular repeatability across bend lengths up to 4,000mm. Automated thickness compensation avoids micro-fractures in high-yield stainless steel alloys.
Our welders are certified according to ISO 9606-1 and ASME Section IX. Robotic orbital TIG and cold-metal-transfer (CMT) welding preserve parent metal properties while preventing burn-through on thin-gauge frame structures.
Following structural fabrication, frames proceed through an automated chemical passivation bath conforming to ASTM A967, which dissolves free iron residues and instantaneously reconstructs the protective chromium oxide passive boundary film. For aesthetic frames, including our minimalist brushed and Bauhaus architectural series, proprietary mechanical polishing creates grain directional satin finishes (Ra < 0.4 µm) or mirror #8 finishes without wave distortions.
Global B2B purchasing dynamics are transitioning rapidly toward supply chain decarbonization, lifecycle cost evaluation, and digital twin engineering integration. Forward-looking procurement directors must anticipate the structural industry shifts shaping global trade over the next decade:
European CBAM (Carbon Border Adjustment Mechanism) regulations are accelerating demand for Electric Arc Furnace (EAF) stainless steel utilizing >85% recycled scrap. Buyers prioritize verified Environmental Product Declarations (EPD).
Procurement teams increasingly integrate cloud-connected parametric 3D STEP models. Direct API submission into automated CNC nesting systems reduces prototype lead times from 4 weeks to 72 hours.
High overseas shipping freights are driving demand for flat-pack knock-down (KD) stainless framing designs with laser-keyed miter tabs, cutting container volume by up to 65% while maintaining on-site rigidity.
Anti-fingerprint (AFP) and PVD (Physical Vapor Deposition) ceramic coatings are replacing traditional electroplating, delivering wear-resistant colors (Titanium Gold, Rose Gold, Black Titanium) with zero heavy metal effluents.
By partnering with an agile manufacturer capable of integrating EPD lifecycle reporting and automated DFM feedback, procurement directors safeguard their capital expenditure against shifting environmental tariffs and logistical bottlenecks.
To fulfill strict CE export parameters, every production run is monitored through an Enterprise Resource Planning (ERP) tracking system linked directly to physical heat numbers. Incoming material undergoes PMI (Positive Material Identification) via handheld XRF analyzers to safeguard against alloy grade mixing. During fabrication, CMM (Coordinate Measuring Machines) verify hole center-to-center distances, diagonal squareness, and weld bead planarity within strict micron tolerances.
Prior to international container packing, structural frames endure rigorous non-destructive testing (NDT), including liquid penetrant inspection (PT) of stress-bearing corner brackets and helium leak testing for enclosed pressure-tight framing skids. For outdoor and architectural hardware, representative samples undergo accelerated ASTM B117 neutral salt spray testing and ASTM G48 ferric chloride pitting tests to validate corrosion longevity in coastal and chlorinated environments.
Export packaging is engineered for trans-oceanic container transport: each frame is isolated with non-staining protective PE film, separated with corrugated shock-absorbing honeycombs, and secured within custom fumigated plywood crates (ISPM 15 compliant) lined with vapor corrosion inhibitor (VCI) desiccants. This rigorous packaging ensures zero moisture staining, edge deformation, or vibration scratch marks during extended maritime transit.
Review comprehensive technical answers addressing common engineering specifications, certification documentation, minimum order quantities, and custom tooling options:
Connect directly with our senior metallurgists and sheet metal fabrication engineers. Receive full DFM feedback, exact factory-direct volume pricing, and custom sample dispatches within 24 hours.